
NewsKnowledges
Among today’s semiconductor components, when choosing materials for dimensional stability and low thermal expansion, cordierite has become one of the choices that cannot be overlooked.
However, machining cordierite into a precision component is not that simple.
Below, I will introduce how Jundro Ceramics machines a blank into a stable component used in semiconductor equipment.
For many structural parts, the machining sequence is:
Rough grinding → CNC machining → Precision grinding
Rough grinding is used first because it removes material much faster than precision CNC milling. A certain amount of allowance is left for CNC machining, so the final dimensions do not depend entirely on the milling operation.
CNC machining is then used for features such as:
After the main features are completed, precision grinding brings the part to its final length and width. This combination works well for components that require both complex geometry and tight dimensional requirements.
The most common difficulty is edge chipping, especially around sharp outer edges, thin walls, small slots and sharp internal corners.
A feature may machine successfully in the main cutting area but still develop a small chip when the tool approaches a sharp edge or breaks through a thin section. Thin-wall structures are particularly sensitive during drilling and slotting because there is less material to support the cutting force.
The machining sequence therefore needs to consider not only the final geometry, but also where material is removed and when vulnerable edges are exposed.
Where the drawing allows it, machining allowance can be left on critical edges and removed during the final grinding operation. In other cases, a chamfer can be introduced to reduce the risk of chipping.
Different operations require different tools.
Diamond grinding tools are mainly used for rough material removal and grinding operations. Their high material-removal efficiency makes them suitable for preparing the blank before detailed CNC machining.
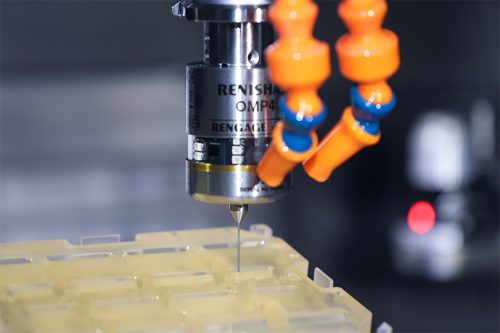
Carbide milling tools are used for precision structural machining. They can produce holes, slots, steps, profiles and other complex features.
The choice is therefore not simply between grinding and milling. The two processes complement each other: grinding handles efficient material removal and dimensional finishing, while CNC milling creates the required geometry.
Small features require considerably more attention than large open surfaces.
A through-hole as small as 0.1 mm in diameter has been machined in low-thermal-expansion cordierite. At this scale, tool condition, cutting direction, material support and edge condition can all affect the result.
Thin-wall structures present a similar problem. During drilling or slotting, the remaining wall may be too weak to tolerate the cutting forces without fracture or chipping. For this reason, the machining sequence and the amount of remaining material are important parts of the process rather than details considered only after the toolpath has been created.
Cordierite machining is not limited to small precision parts. At Jundro Ceramics, we can process components up to approximately 500 × 500 mm, including complex structural components, semiconductor equipment parts and mirror-type components.
For larger precision parts, temperature consistency also becomes relevant. Although cordierite has very low thermal expansion, temperature can still affect machining and dimensional inspection. For this reason, we pay attention to temperature consistency during CNC machining, grinding and inspection to help keep the result consistent from one stage to the next.
| Dimension Capability | Cordierite |
|---|---|
| Maximum Size | 500 × 500 mm |
| Flatness | 0.001 mm (Φ300) |
| Concentricity | 0.005 mm |
| Cylindricity | 0.001 mm |
| Parallelism | 0.001 mm |
| Minimum Wall Thickness | 0.1 mm |
| Minimum Hole Diameter | Ø0.1 mm |
| Minimum Slot Width | 0.2 mm |
| Minimum Internal Thread | M1.6 |
| Polishing | Ra 0.02 μm |
The actual achievable tolerance depends on the cordierite grade, component size, geometry, wall thickness, feature position and drawing requirements.
For low-thermal-expansion cordierite, successful machining is less about using a single “special” machining method and more about controlling the sequence: remove material efficiently, machine the geometry carefully, protect fragile edges, and use precision grinding for the final dimensions.
If you have a drawing or specific cordierite machining requirements, please send them to us. We can review the design and evaluate the machining feasibility based on your requirements.


Chinese (Simplified)

English

German

Japanese

Spanish
Floors 1-2, Building 3, Qianyuan Industrial Park, No. 2 Gaoxin 2nd Road, Dalang Town, Dongguan, Guangdong, China(523770)